
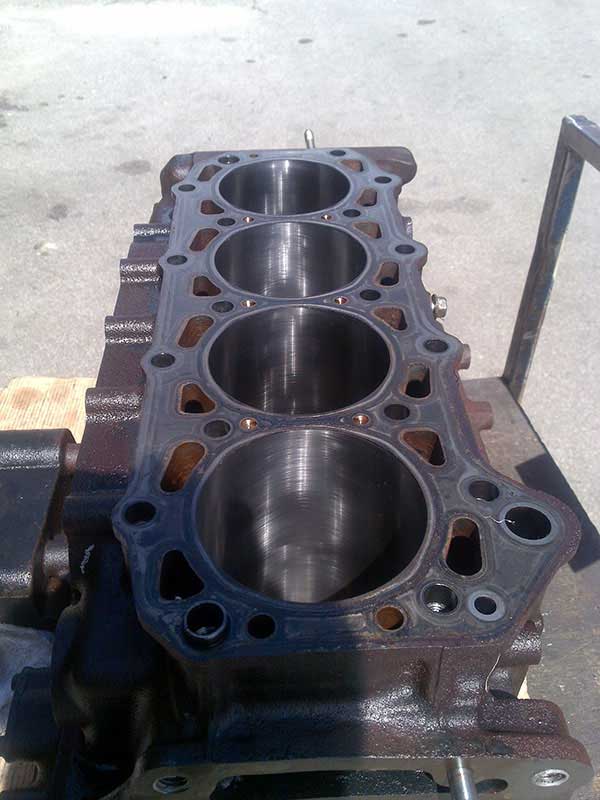
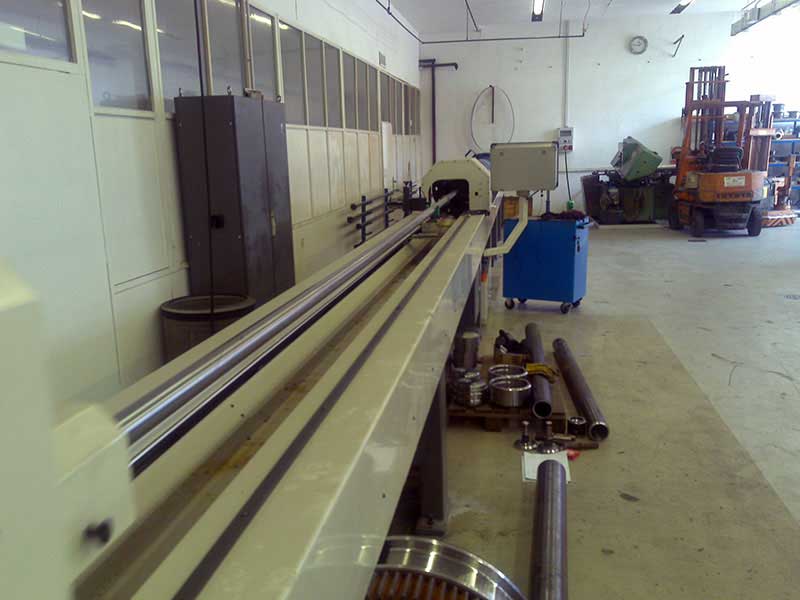
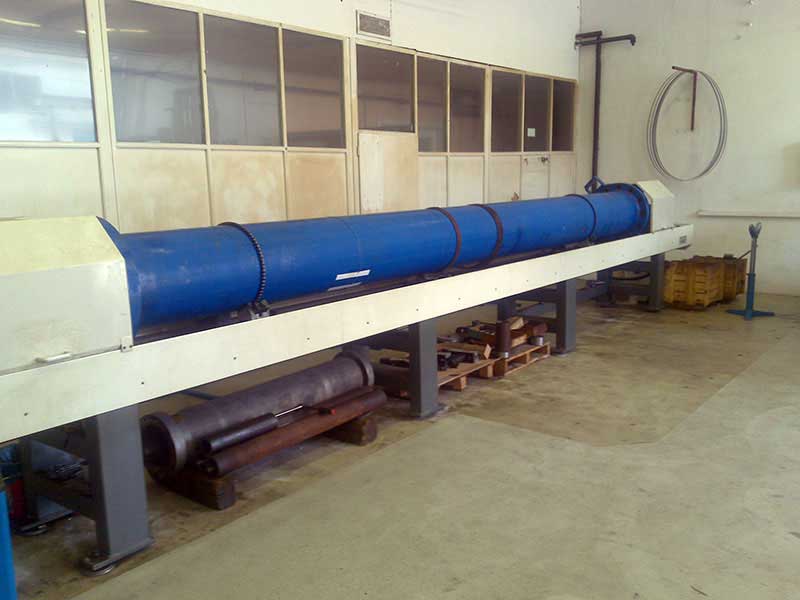
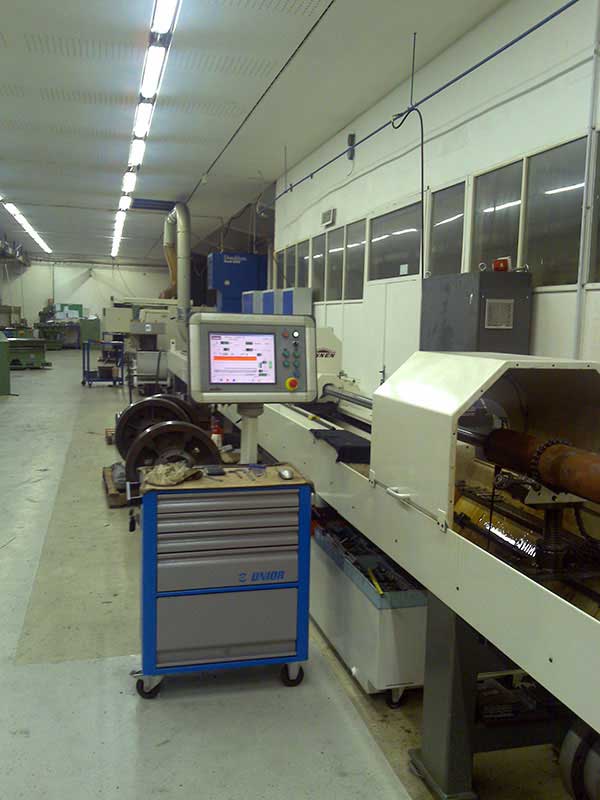
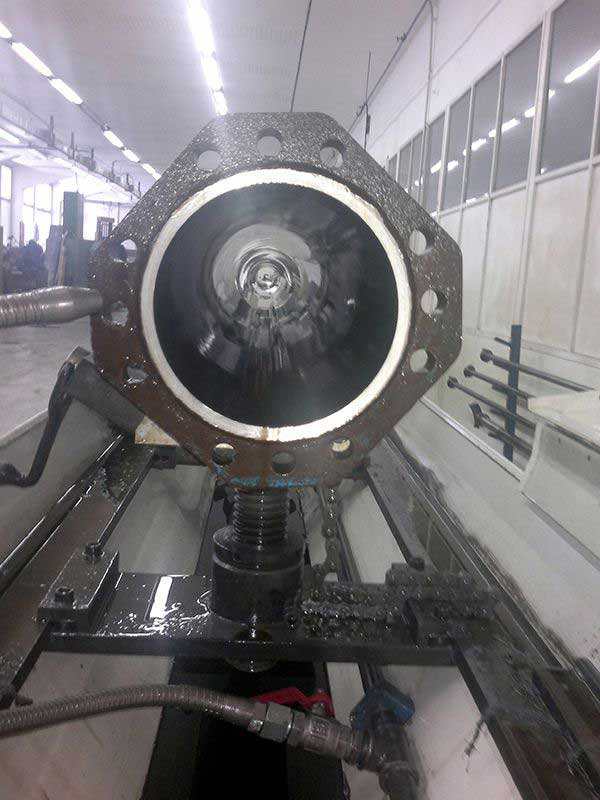
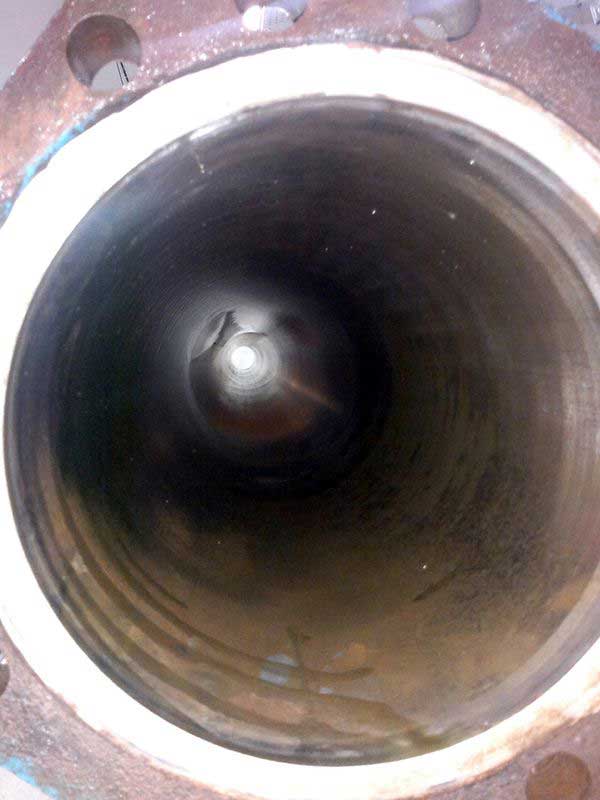
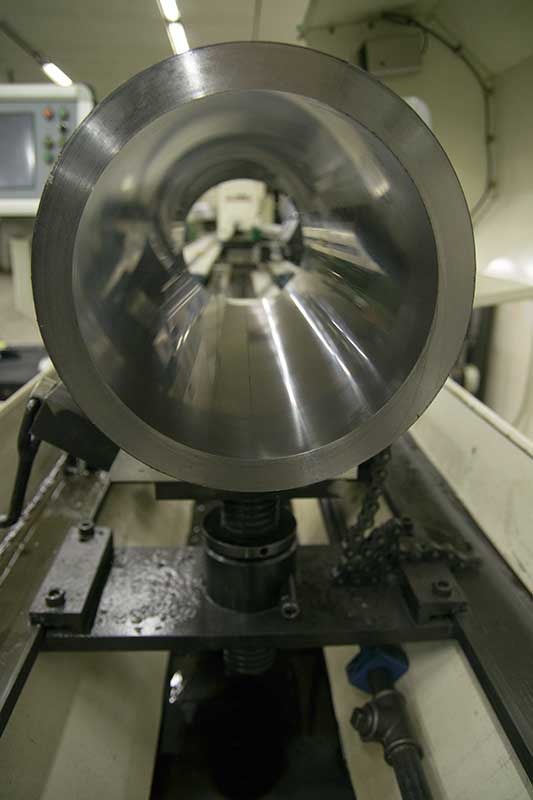
Honing is a fine machining process by cutting. It is similar to fine grinding, in which the workpiece does not heat up in contact with the tool, so the structure of the machined surface does not change.
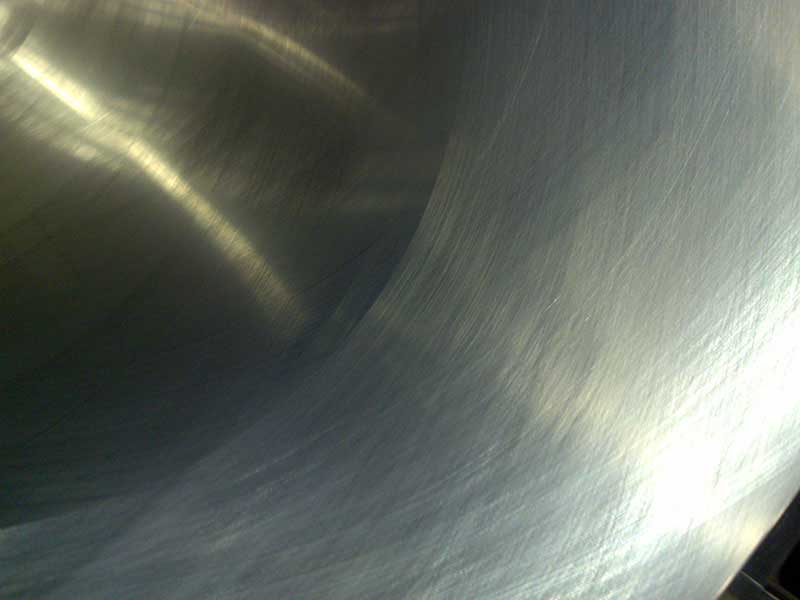
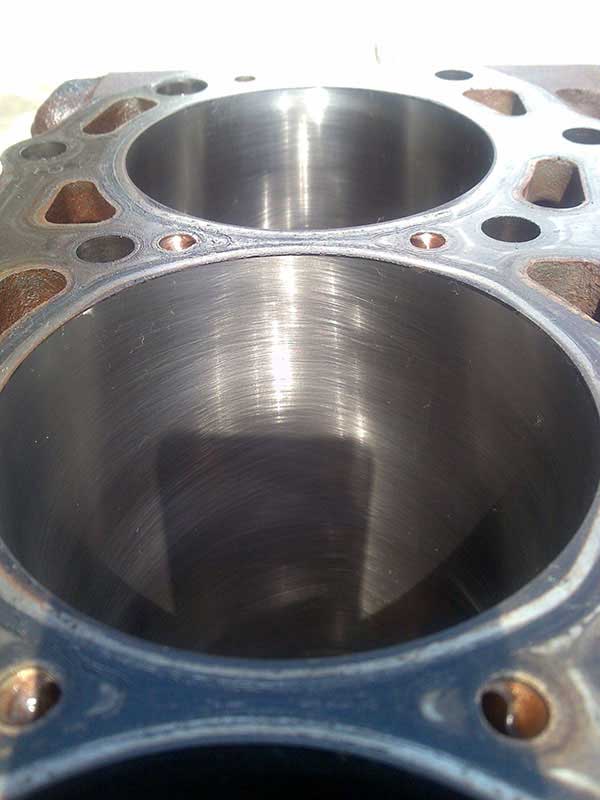
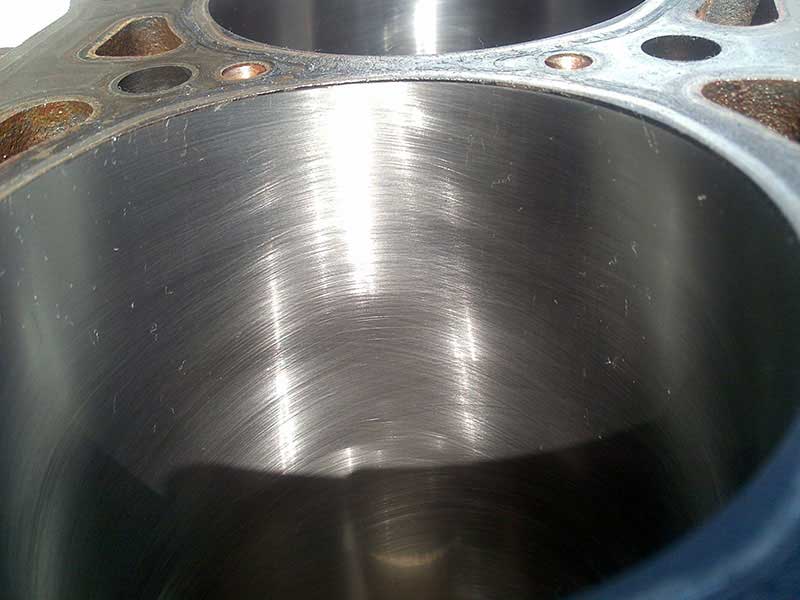
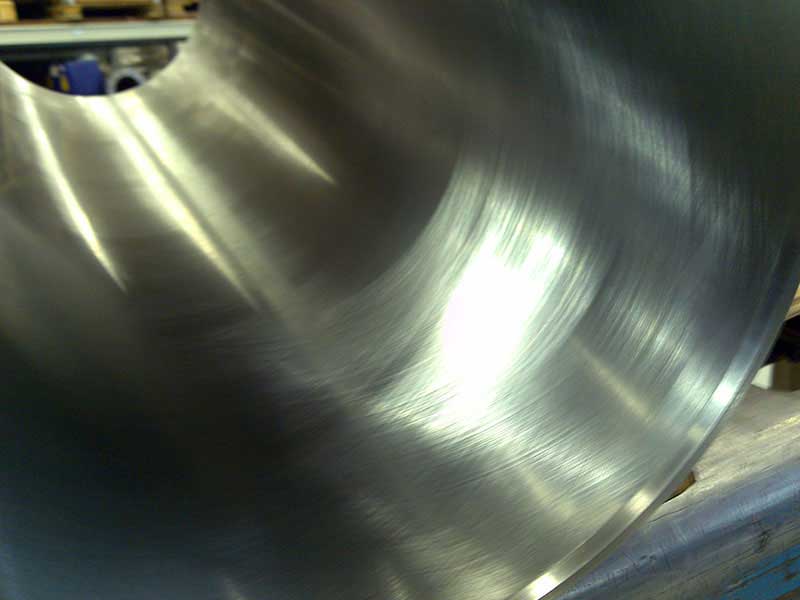
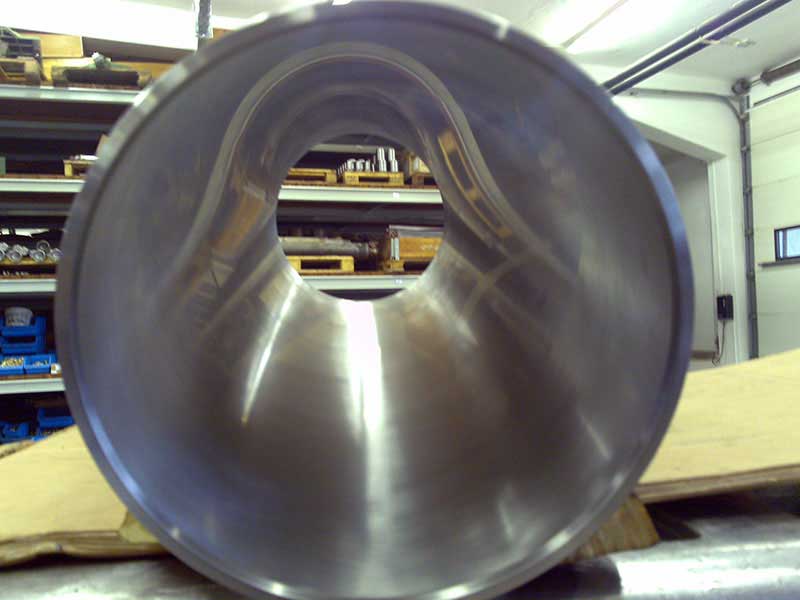
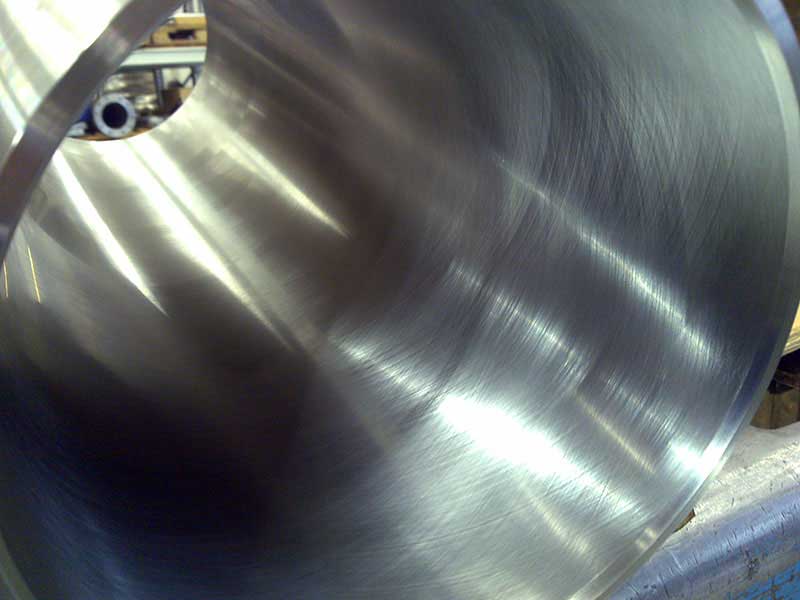
The main difference between honing and grinding is the considerably lower tool speed in honing. The tool contacts the workpiece over a large area, so the surface pressures are much lower than in grinding and the chip cross-section is small; the result is an exceptionally smooth finish with a slightly matt surface.
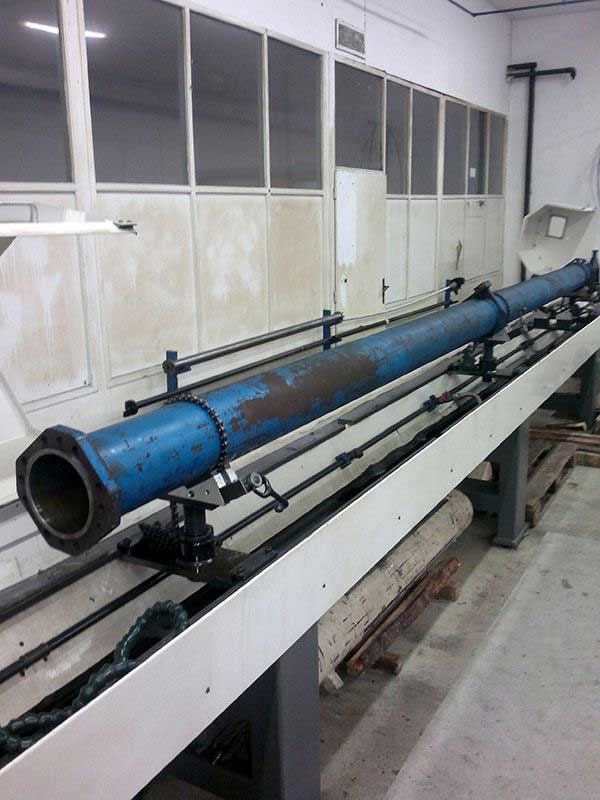
Compared with a rolled tube, internal honing ensures a longer cylinder life. A hydraulic cylinder also distorts after each weld on the tube (connections, mountings); with this technology we remove these deformations and ensure the roundness of the tube, which significantly reduces cylinder service costs.
HONING CAPABILITIES
Our capabilities
Surface roughness
Bore diameter
Length
PHOTOS
Gallery
VIDEO
Internal honing in practice
Do you need honing?
Get in touch and we will find the best solution for your project.